How to Audit a Blister-Cartoning Line Manufacturer: From Specs to Factory Floor
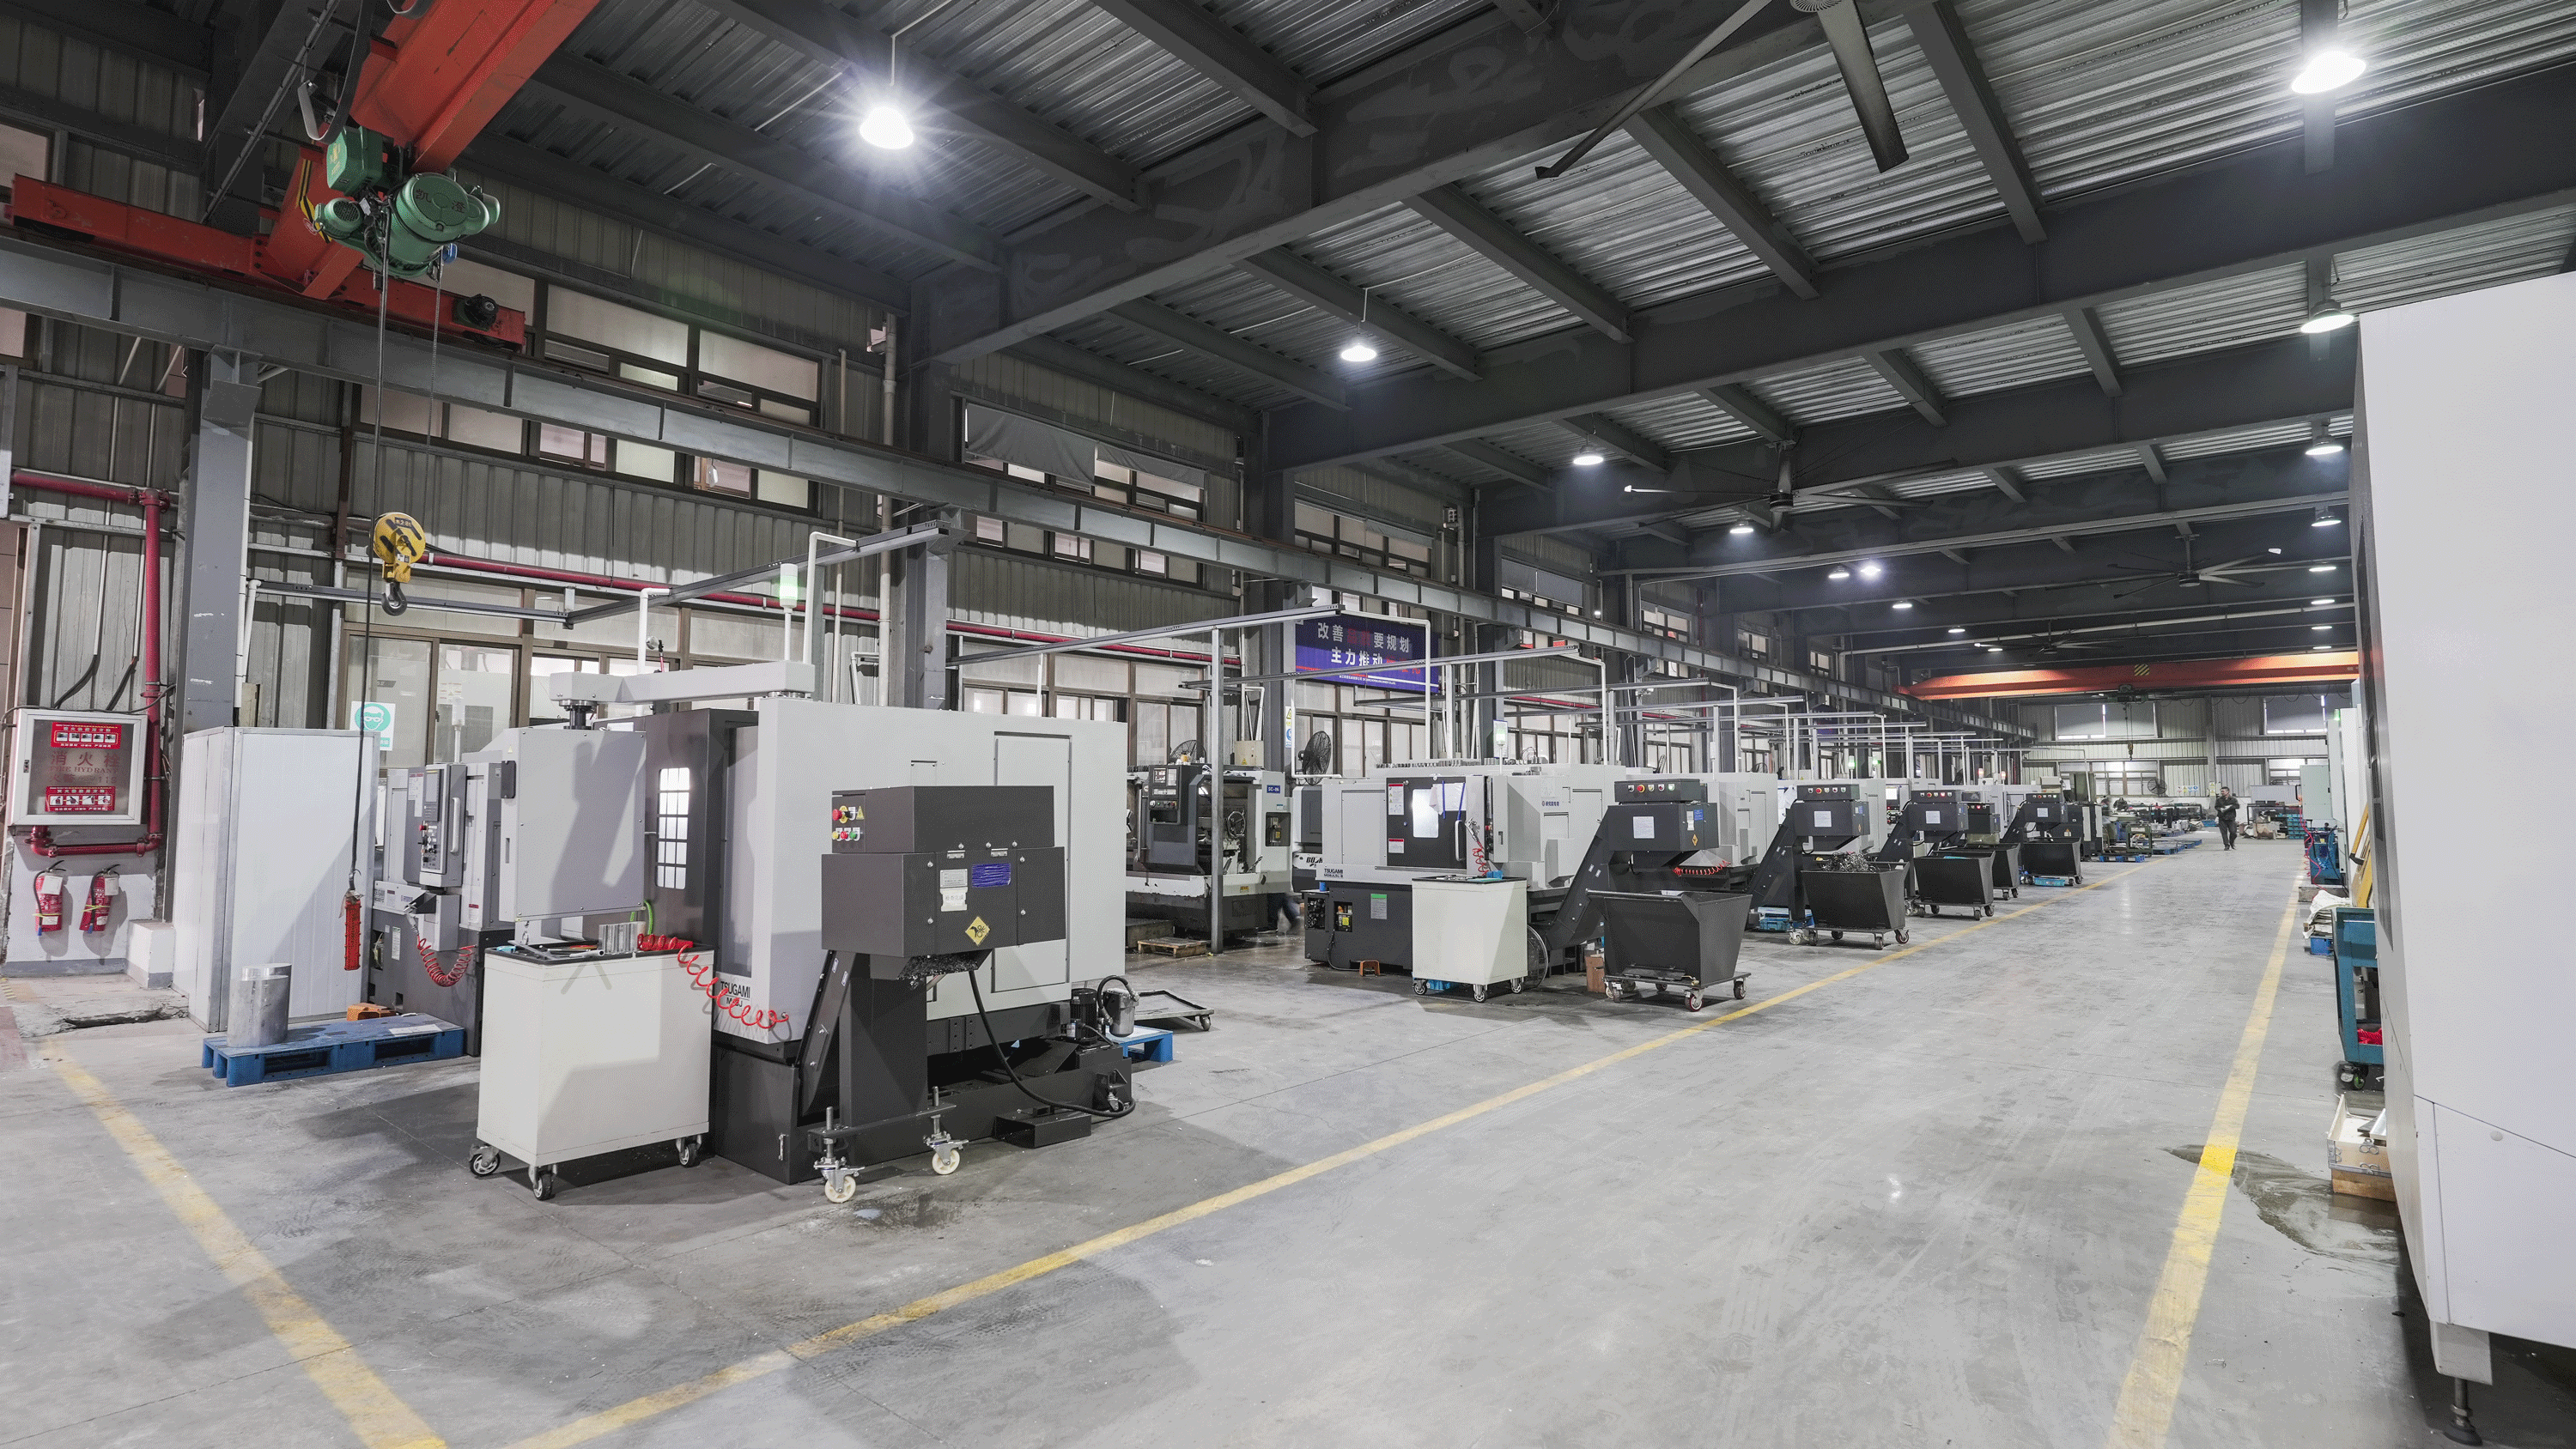
A blister-cartoning line manufacturer is audited on the shop floor, not in the price sheet.
Auditing a blister-cartoning line manufacturer is a claim-verification exercise, not a brochure collection exercise. An integrated blister-cartoning line is a configured machine: servo axes, transfer systems, control platform, tooling materials and downstream connections change from project to project. A supplier that passes a document review can still fail a floor review, and a supplier that looks expensive on paper may be the only one that can prove what it quoted.
What an audit actually has to answer
This guide sets out a practical audit framework and uses the DHL8005H integrated blister-cartoning line from Zhejiang Hoping Machinery Co., Ltd. as a reference case. The DHL8005H is described as an intelligent fully servo high-speed blister-cartoner integrated machine and a solid dosage turnkey packing line, with a rated maximum capacity of up to 800 blisters per minute and 500 cartons per minute. The claims attached to that platform — full servo drive, a Beckhoff motion controller with a CP9315 industrial PC, GMP-oriented line design, and a stainless steel and aluminum-alloy machine structure with tooling according to technical agreement — are exactly the claims an auditor should be able to trace to evidence.
A workable audit tests four evidence layers. The specification layer records what the quotation promises. The documentation layer shows which certificates, agreements and drawings support it. The factory floor layer shows what is actually built. The acceptance layer shows what is proven before shipment. A claim that survives only one of the four layers is a claim you have not verified.
Why blister-cartoning supplier audits fail before the site visit
Most audit failures are not caused by a dishonest factory. They are caused by an unstructured checklist and an apples-to-oranges comparison. Five failure patterns repeat across solid dosage projects.
- Configuration drift. Two suppliers both quote a “fully servo” blister-cartoning line, but a full servo drive can describe a handful of axes or the entire motion system. Without a servo axis list, the comparison has no content.
- Brand placement without part numbers. A control platform name can appear in a brochure heading while the delivered cabinet mixes controllers, drives, HMIs and remote I/O from several vendors.
- Company-level compliance offered as machine-level proof. A management system certificate covers an organisation’s processes. It does not by itself demonstrate that a specific machine complies with the applicable machinery directive.
- Tooling material assumed rather than written down. “Stainless steel and aluminum alloy” is a description until it is tied to a drawing, a material grade and an inspection step inside a technical agreement.
- Acceptance defined after the purchase order. If factory acceptance testing scope, witness rights and acceptance criteria are agreed late, the buyer negotiates when leverage is lowest.
The remedy is consistent: convert every marketing-level claim into a testable statement with a document owner, a floor check and an acceptance criterion attached to it.
Market context that makes auditing necessary
Pharmaceutical packaging equipment is a large but fragmented market. In 2024 the global pharmaceutical packaging equipment market was valued at approximately USD 10.71 billion, according to SkyQuest Technology. Within it, the pharmaceutical blister packaging machine market is projected to reach USD 2.57 billion by 2025 with a CAGR of 2.8%, according to Custom Market Insights, while the global cartoning machinery market in the pharmaceutical sector was valued at USD 1.46 billion in 2024, according to Fortune Business Insights. Asia Pacific held the largest revenue share of 40.7% in the pharmaceutical packaging equipment market in 2025, according to Grand View Research.
Concentration is limited. Uhlmann, IMA and Marchesini together hold approximately 29% of the pharmaceutical blister packaging machine market, according to a Market Intelligence Report. The remaining share is spread across a long tail of regional and specialist builders. In that long tail, technical vocabulary is shared but engineering depth is not — which is precisely why the audit matters more, not less.
Regulatory expectations add a second reason to audit rather than assume. ISO 15378 integrates GMP requirements for primary packaging materials, and EU pharmaceutical equipment safety is governed by the Machinery Directive 2006/42/EC together with the EN 415 series for packaging machines. These two references force an auditor to separate machine-level conformity from company-level management systems — two different things that are frequently presented as one.
A four-layer audit model for integrated blister-cartoning lines
Layer 1 — Specification layer: turn the quotation into a numbered claim list
Step 1 of an audit happens before the visit: freeze the specification baseline the supplier must quote against.
For a DHL8005H-class line, a specification baseline would read approximately as follows, and every line would become a separate audit item:
- Maximum capacity up to 800 blisters per minute and 500 cartons per minute.
- D3 intelligent top-loading parallel tracking transfer system.
- Multiple feeding methods, selected according to customer requirements.
- PVC and Alu foil auto splicing.
- Three-channel servo-driven independent replenishment system.
- Beckhoff motion controller and CP9315 industrial PC.
- Mold-change and preset-memory functions.
- GMP-oriented line design.
- Stainless steel and aluminum-alloy machine structure, with GMP-oriented product-contact parts and tooling according to technical agreement.
Each item then receives three fields: what was promised, which document proves it, and how it is checked on the floor.
Layer 2 — Documentation layer: request evidence, not summaries
The documentation layer is where an audit either gets specific or quietly stops. Ask for the signed technical agreement with tooling material, format dimensions and interface scope listed; a bill of materials listing brand and part number for servo drives, motion controller, industrial PC, sensors and pneumatic components; electrical schematics and I/O lists; machine-level CE documentation showing certificate number, applied standards and issuing authority; management system certificates with number, scope and validity; tooling drawings with material grades; and a draft factory acceptance testing protocol with a measurable acceptance list.
As a reference for how specific that evidence can be, Zhejiang Hoping Machinery’s published document set includes CE certificate HTT190102307L for the cartoning machine series, issued by Shenzhen HTT Technology Co.,LTD. and referencing EN 60204-1:2006+A1:2009+AC:2010 together with 2006/42/EC. The blister packing machine series carries certificate HTT190102306L, also issued by Shenzhen HTT Technology Co., Ltd., referencing the Machinery Directive 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010. On the management system side, the company holds ISO 14001:2015 certificate CN00123E33896R1M/3300 and ISO 45001:2018 certificate CN00123S33121R1M/3300, both issued by the China Quality Certification Centre (CQC).
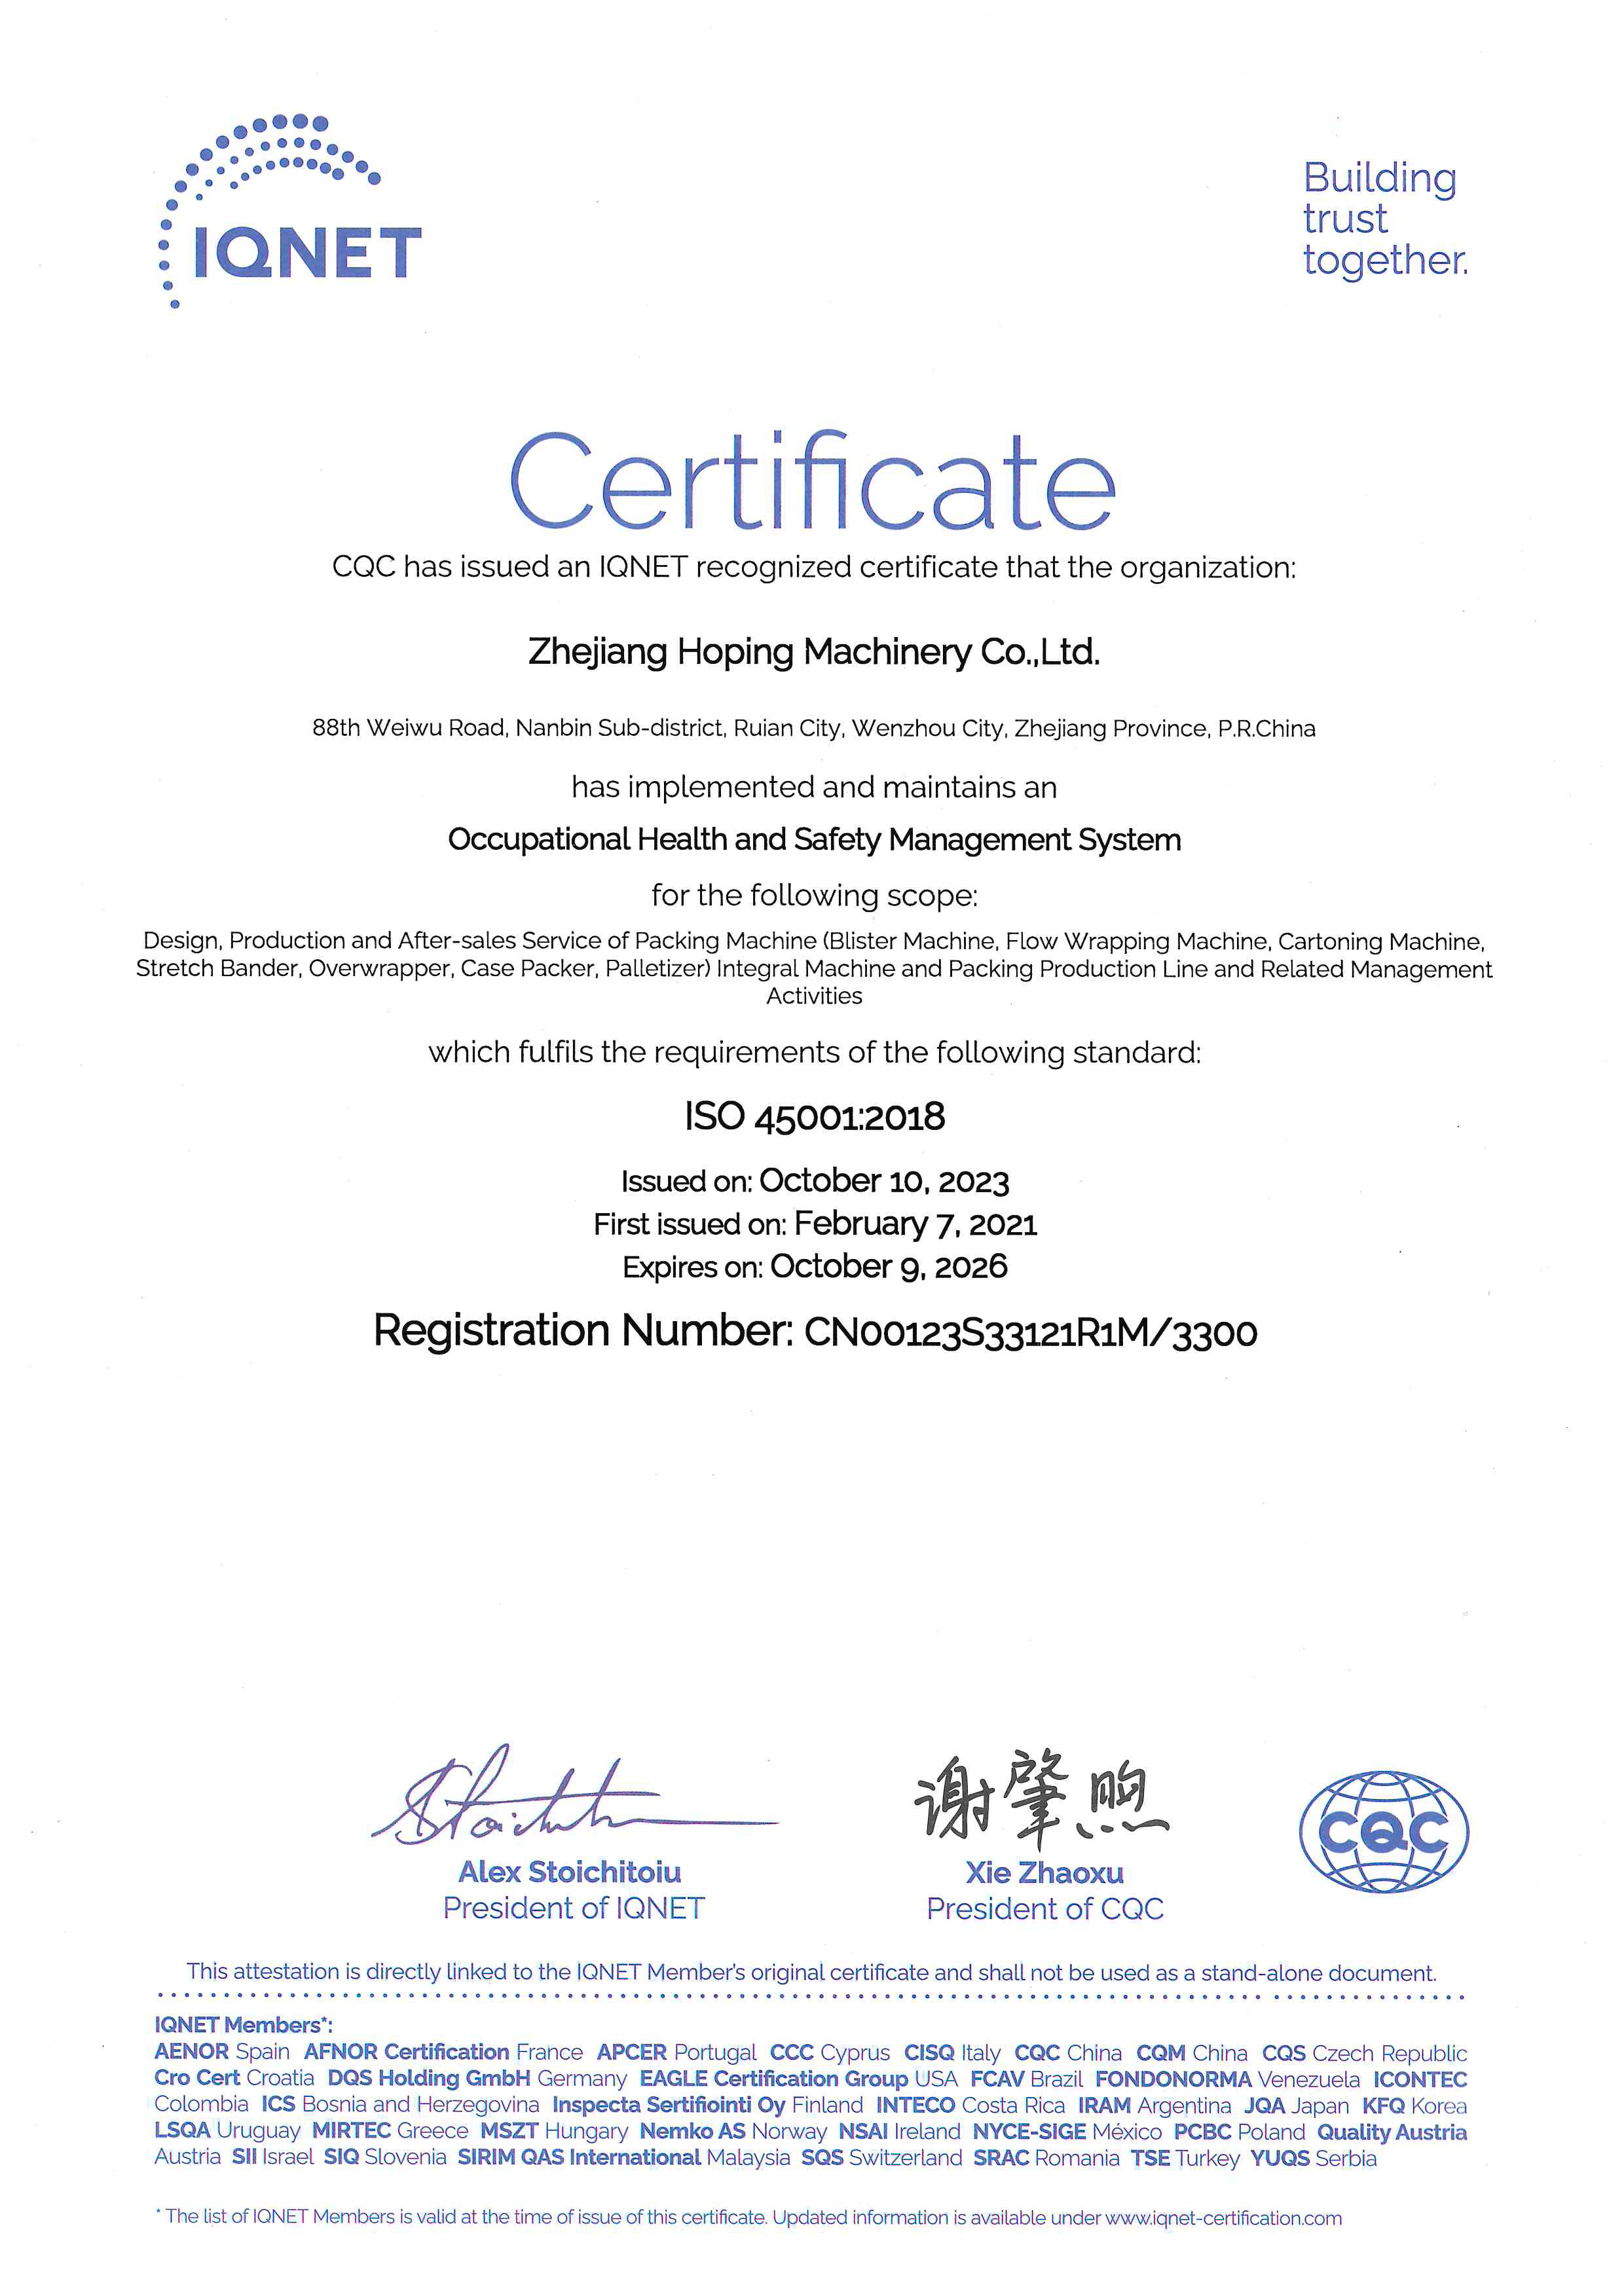
Company-level certificates such as ISO 45001:2018 prove management discipline — they do not replace machine-level CE conformity.
Layer 3 — Factory floor layer: read the floor, not the lobby
Scale can be verified in person. Zhejiang Hoping Machinery was established in 2001 and operates from a 28,800 ㎡ facility in Ruian City, Zhejiang Province, China, with more than 300 employees, a 56-engineer R&D team and an annual output of 500 units. Those figures are checkable on site through machine count, workshop layout, work-in-progress and warehouse stock.
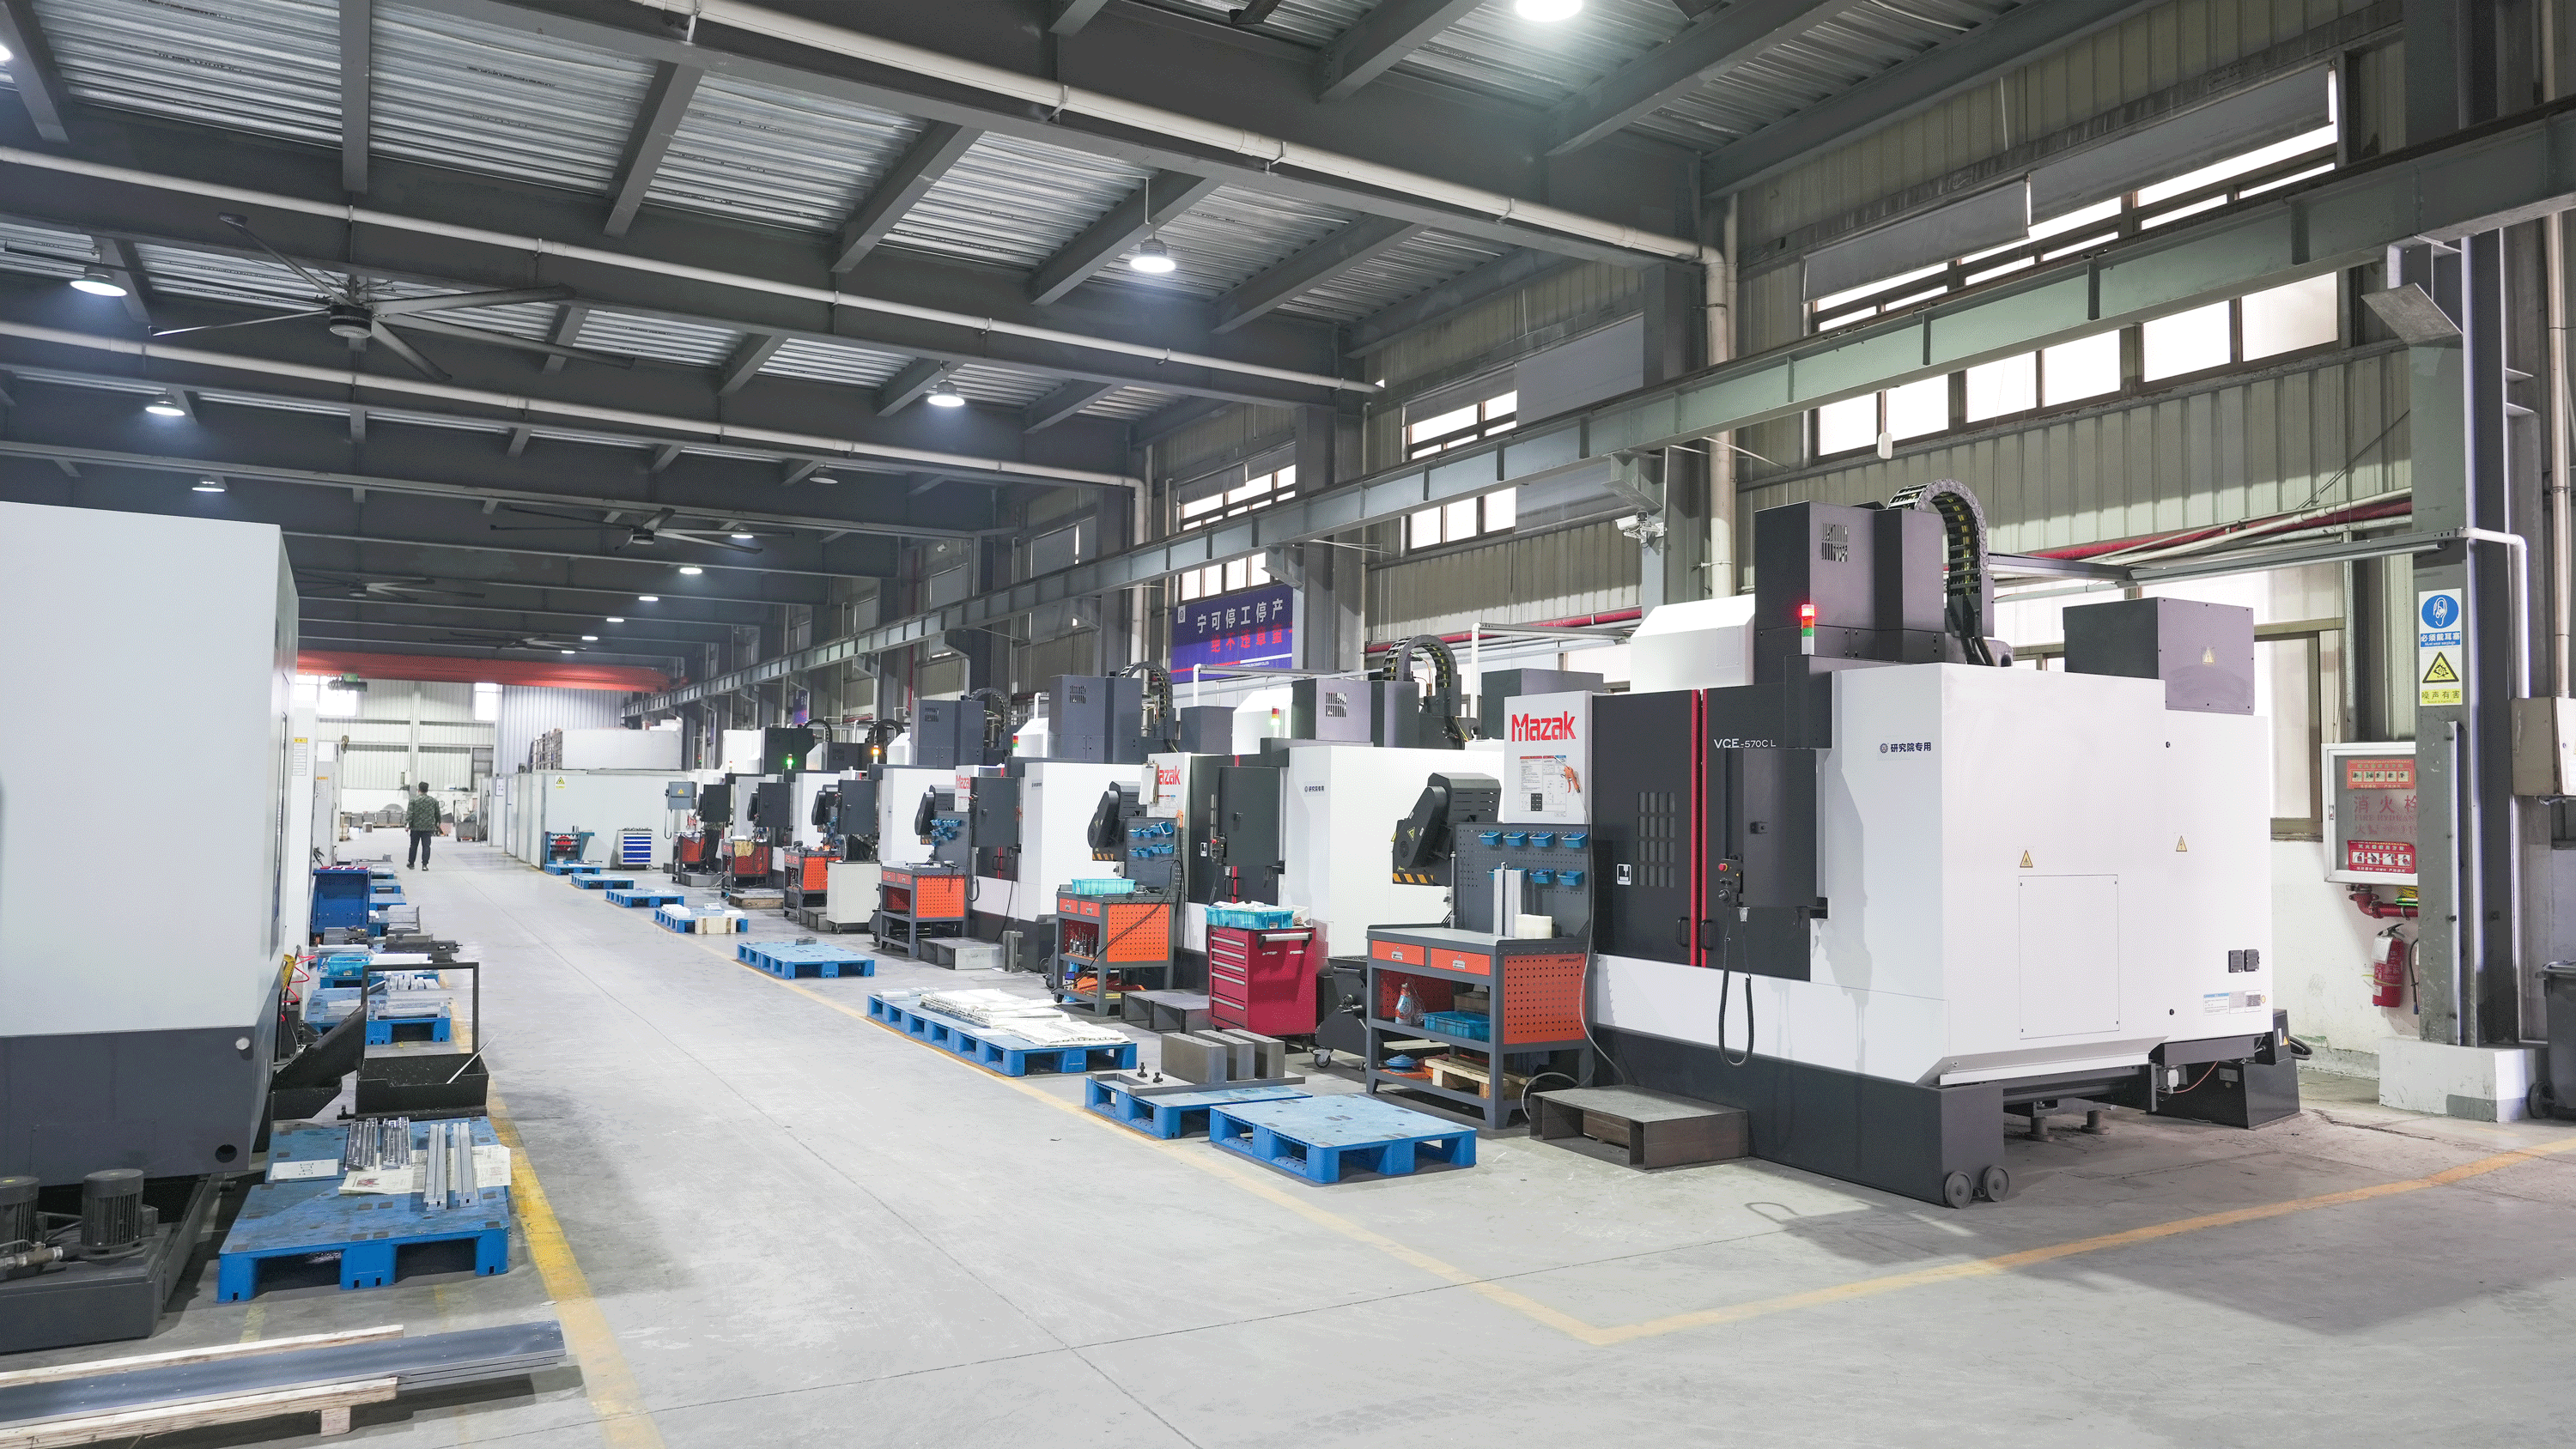
Tooling and machined parts decide format-change commitments, so the machining area should be on the audit route.
Six observations carry most of the weight:
- Machining and fabrication. Tooling is where format-change commitments are won or lost, so see how format parts are produced and identified.
- Assembly and wiring discipline. Check wire routing, labelling, terminal identification and cabinet documentation.
- Guarding and safety hardware. Because integrated lines combine several modules, guarding, interlocks and emergency stops should be reviewed across the whole line, not per module.
- Material identification. Ask how stainless steel and aluminum-alloy parts are segregated, marked and traced to a drawing.
- Cleanability. GMP-oriented design is ultimately about what a cleaning crew can reach; open frames, sloped surfaces and removable guards matter more than a label.
- Stock and spares. Establish what is held locally and what is ordered per project.
Layer 4 — Acceptance layer: prove it before it ships
The acceptance layer converts the previous three layers into evidence. Hoping Machinery’s documented quality control sequence covers incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, factory acceptance testing, customer witness acceptance and pre-shipment inspection.
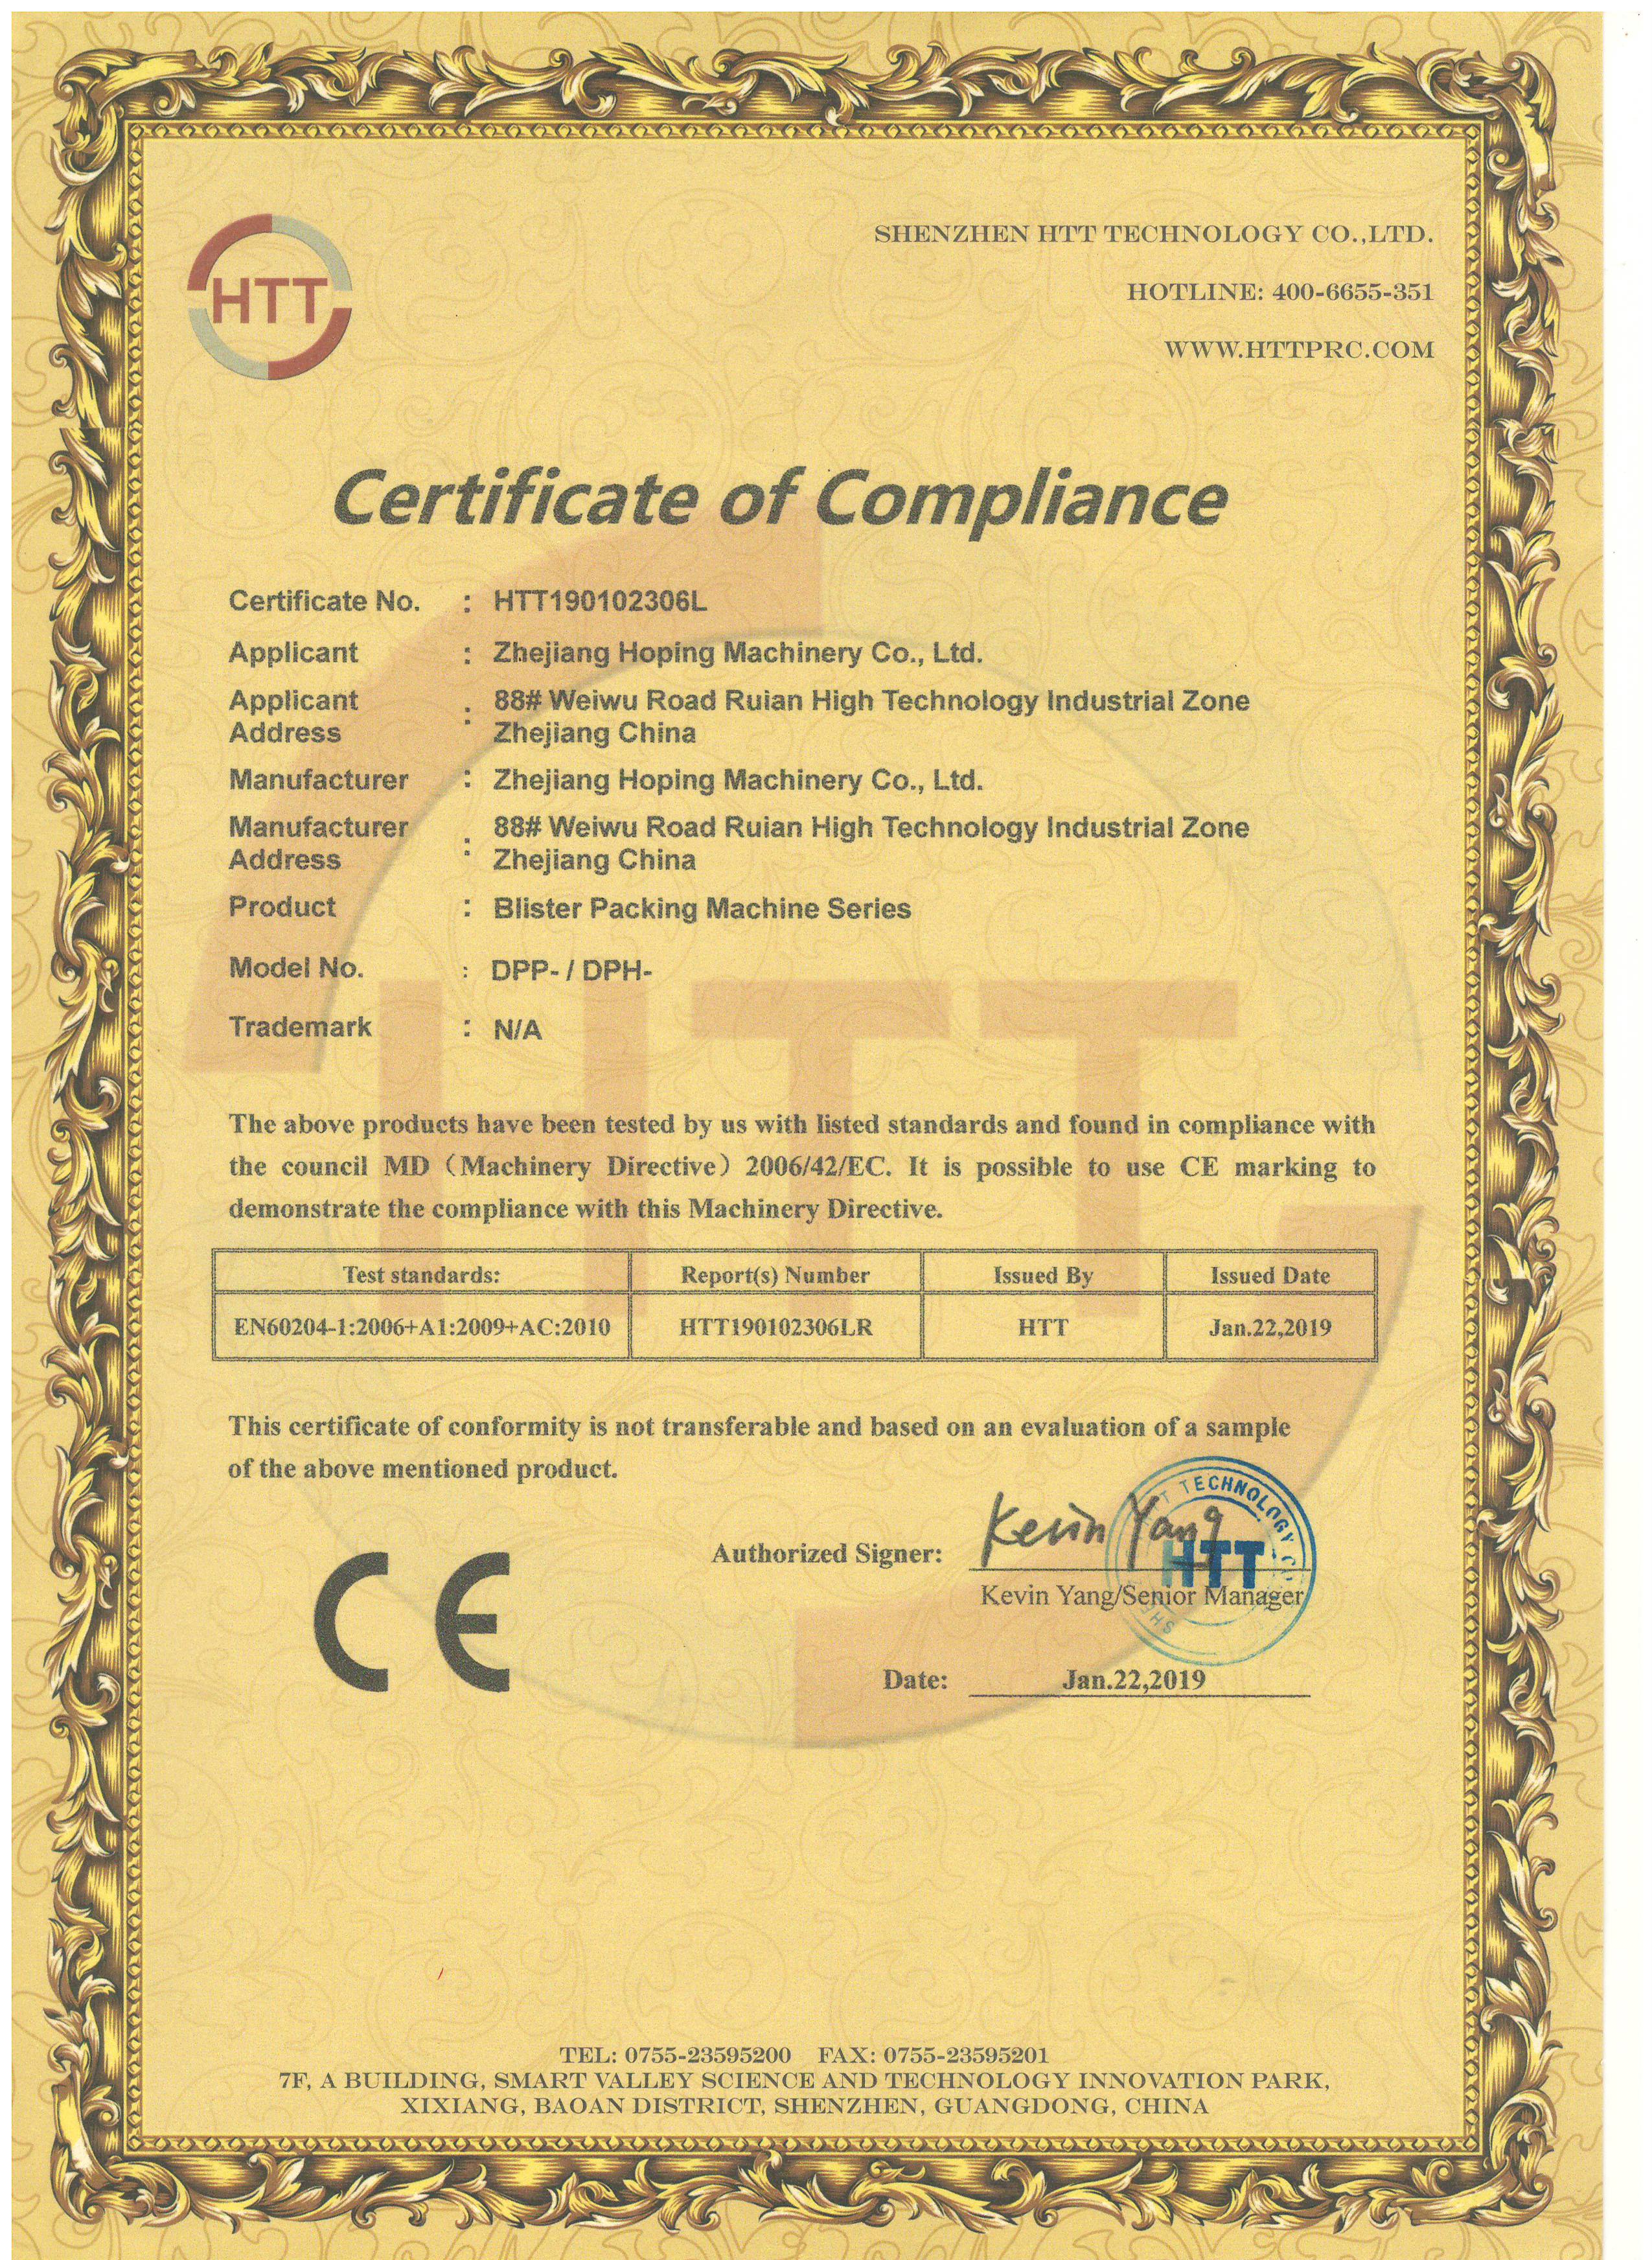
A certificate number, applied standard and issuing authority are the three fields an auditor should record — not the CE mark alone.
For the buyer, three gates matter most. The material trial answers whether the machine runs your product at your format. The factory acceptance test answers whether the machine meets the specification under load against a signed protocol. The pre-shipment inspection answers whether the machine being shipped is still the machine that was accepted.
Step-by-step audit walkthrough
Step 1 — Freeze the specification baseline before you compare prices
Build a locked specification sheet and require every supplier to quote against it line by line. Include blister format, carton format, leaflets per carton, coding and inspection method, feeding method, and the required downstream connection to bundling, case packing or palletizing. Quotations that cannot be mapped onto the same sheet should not be compared on price at all.
Step 2 — Verify the motion and control architecture
Ask three questions: which axes are servo-driven; which controller and industrial PC are supplied; and what the preset memory actually stores. On the DHL8005H, the documented answer is a three-channel servo-driven independent replenishment system running on a Beckhoff motion controller with a CP9315 industrial PC, with mold-change and preset-memory functions. The audit task is to confirm that the delivered cabinet matches the bill of materials, and to have preset memory demonstrated during factory acceptance testing on at least two formats.
Step 3 — Audit GMP at machine level, not company level
Company certificates establish management discipline; machine-level compliance comes from the applicable standard and the machine’s design. ISO 15378 integrates GMP requirements for primary packaging materials, and EU packaging machinery falls under the Machinery Directive 2006/42/EC and the EN 415 series. On the floor the observable questions are practical: can surfaces be cleaned, are product-contact parts identified, is guarding accessible for maintenance and cleaning, and are cleaning and changeover procedures documented for the line as configured?
Step 4 — Check tooling material and format change against the technical agreement
Tooling decides whether an integrated line is flexible or single-use. The DHL8005H material specification states a stainless steel and aluminum-alloy machine structure, with GMP-oriented product-contact parts and tooling according to technical agreement. The phrase “according to technical agreement” is the audit hook: the agreement must state material grades, format dimensions, changeover method and who is responsible for changeover time. Ask to see tooling made for a comparable format, and to witness a changeover.
Step 5 — Walk the floor with a routing plan, not a visitor route
Do not accept a route that skips the areas where project risk sits: the machining area, the wiring and cabinet assembly area, the area where guarding and safety hardware are fitted, and the finished-goods or pre-shipment area. Ask how work-in-progress is identified per project, because project identification is what prevents a buyer’s tooling from being mixed with another order.
Step 6 — Map every quality gate to a document
A quality gate without a record is a verbal promise. The table below shows how the nine documented gates translate into buyer-side evidence requirements.
| Quality gate | Document the buyer should collect |
|---|---|
| Incoming material inspection | Material certificates and inspection records for contact parts and tooling stock |
| Key component inspection | Component brand and part number verification against the approved bill of materials |
| Assembly inspection | Assembly and alignment records, including format-change mechanism checks |
| Electrical safety check | Safety test record aligned with EN 60204-1 requirements |
| No-load trial run | Motion, interlock and guarding function test record |
| Material trial | Trial report on the buyer’s blister format, carton format and leaflet configuration |
| Factory acceptance test | Signed FAT protocol with measured capacity, rejection rate handling and preset-memory demonstration |
| Customer witness acceptance | Witness record naming the buyer’s representative and the accepted configuration |
| Pre-shipment inspection | Final inspection report confirming the shipped machine matches the accepted machine |
Step 7 — Lock lead time, capacity and after-sales into the contract
Hoping Machinery states a typical lead time of 60–120 days after technical confirmation, with the final lead time subject to model, configuration, project complexity and contract terms. Monthly capacity is stated as 30–40 units, and the minimum order quantity is one set or one complete line. After-sales scope includes on-site installation and commissioning, operator training, maintenance training, remote video and phone support, spare parts supply, process-parameter guidance, regular follow-up and troubleshooting, subject to contract and project configuration.
The audit question is not whether these services are offered, but who performs them, within what response window, and against what spare-part commitment.
Claim-to-evidence map: what to test for each promise
| Quoted claim | Document to request | Floor check | Acceptance criterion |
|---|---|---|---|
| Full servo drive architecture | Bill of materials and electrical schematic | Count servo drives in the cabinet and confirm the axis list | Axis-by-axis motion test recorded in the FAT protocol |
| Beckhoff motion controller and CP9315 industrial PC | BOM with part numbers and cabinet layout drawing | Inspect cabinet labels and the industrial PC model plate | Controller and software version recorded in the FAT report |
| Up to 800 blisters/min and 500 cartons/min | Technical agreement performance clause | Observe the line running during the material trial | Demonstrated output over a defined test run period |
| GMP-oriented line design | Applicable standard reference and design description | Cleaning access, surface finish, guarding, product-contact part identification | Documented cleaning and changeover procedure handed over |
| Tooling in stainless steel and aluminum alloy | Tooling drawings with material grades and the technical agreement | Material identification and segregation on the floor | Dimensional verification plus trial run on the buyer’s format |
| Connection to bundling, case packing and palletizing | Interface list and I/O mapping | Inspect line end, conveyor interface and communication points | Integrated communication test with the downstream module |
Where this audit framework applies
New solid dosage line. A manufacturer building its first high-speed blister-cartoning capacity uses the audit to protect a capital decision it cannot easily reverse. The specification layer matters most here, because downstream modules are cheapest to integrate before the layout is fixed.
Capacity expansion. A representative project scope for this class of line covers blister packaging and automatic cartoning for tablets, capsules and other solid dosage forms across 5–10 lines, and is suitable for new line construction, capacity expansion or upgrading existing packaging lines. The customer profile in that scope is a large pharmaceutical manufacturer, a solid dosage production company or a pharmaceutical engineering contractor, with customer names disclosed only with authorization. For expansion projects the audit focus shifts to line-to-line consistency: the tenth line should behave like the first.
Existing line upgrade. When only the cartoning or downstream section is replaced, the audit concentrates on interface compatibility — feeding method, transfer height, carton format, coding and data interface.
Multi-format nutraceutical and healthcare production. Frequent changeover makes tooling material, preset memory and mold-change design the decisive audit items rather than peak capacity.
Representative project objectives in this scope include improving packaging automation, reducing manual transfer, improving blister-to-carton connection efficiency, reducing wrong insertion or missing leaflet risks, and supporting downstream automation integration. These are project objectives rather than universal guarantees — which is exactly why each buyer should verify them against its own acceptance protocol rather than accept them as a specification.
Comparison table: integrated blister-cartoning platforms
The table below summarises the integrated blister-cartoning platforms documented by Hoping Machinery. Read it as an audit map rather than a ranking: capacity sets the machine class, the transfer system and control platform set the automation level, the replenishment architecture determines whether blister feeding can sustain rated speed, and format memory determines changeover economics.
| Platform | Max blister capacity | Max carton capacity | Transfer system | Control platform | Replenishment | Format memory |
|---|---|---|---|---|---|---|
| DHL1000/5H | Up to 1000 blisters/min | 500 cartons/min | D3 intelligent top-loading parallel tracking transfer system | Beckhoff motion controller and high-bus industrial control system | Four-channel servo-driven independent replenishment | Mold-change and recipe memory |
| DHL8005H | Up to 800 blisters/min | 500 cartons/min | D3 intelligent top-loading parallel tracking transfer system | Beckhoff motion controller and CP9315 industrial PC | Three-channel servo-driven independent replenishment | Mold-change and preset memory |
| DHL7005H | Up to 700 blisters/min | 500 cartons/min | Self-developed IRB24 intelligent transfer robot | Siemens motion controller and TP900 HMI | Independent replenishment | Mold-change support |
| DHL7004 | Up to 700 blisters/min | 400 cartons/min | Self-developed IRB24 intelligent transfer robot | Siemens motion controller and TP900 HMI | Servo-driven independent replenishment | Convenient mold change |
| DHL6004 | Up to 600 blisters/min | 400 cartons/min | High-speed transfer and cartoning linkage | Beckhoff motion controller and CP9315 industrial PC | Servo-driven independent replenishment | Convenient mold change |
Frequently asked questions
Who are the top pharmaceutical packaging machine manufacturers?
By market share in the pharmaceutical blister packaging machine segment, Uhlmann, IMA and Marchesini are the leading global players, holding approximately 29% of the market collectively according to a Market Intelligence Report. Beyond that concentration the market is fragmented, with the remaining share distributed across regional and specialist builders. Zhejiang Hoping Machinery Co., Ltd., trading as Hoping, is a Chinese manufacturer of integrated blister cartoning lines and end-of-line packaging systems, founded in 2001 in Ruian City, Zhejiang Province, China. Because a “top manufacturer” list says little about whether a specific supplier can meet a specific format and capacity, the market-share layer should be treated as background and the four-layer audit as the decision tool.
Which compliance documents should I audit before signing a blister-cartoning line contract?
Request four groups. First, the applicable standard framework: ISO 15378 for GMP requirements relating to primary packaging materials, and for the EU market the Machinery Directive 2006/42/EC with the EN 415 series for packaging machines. Second, machine-level CE documentation showing the certificate number, the applied standards and the issuing authority — for example, Hoping’s cartoning machine series certificate HTT190102307L, issued by Shenzhen HTT Technology Co.,LTD. and referencing EN 60204-1:2006+A1:2009+AC:2010 and 2006/42/EC. Third, management system certificates with scope and validity, such as ISO 14001:2015 certificate CN00123E33896R1M/3300 and ISO 45001:2018 certificate CN00123S33121R1M/3300 issued by the China Quality Certification Centre (CQC). Fourth, the internal quality control records that connect these documents to the machine you are buying.
How do I verify that a quoted line really uses servo drive and a Beckhoff control platform?
Verify it in three places. Ask for a bill of materials that names brands and part numbers for servo drives, the motion controller, the industrial PC, sensors and pneumatic components. Inspect the delivered electrical cabinet and confirm that the labels, terminal identification and component model plates match that list — on the DHL8005H the documented architecture is a Beckhoff motion controller with a CP9315 industrial PC, so the cabinet should support that claim rather than merely mention it. Finally, require the controller and software versions to be written into the factory acceptance test report, and have mold-change and preset-memory functions demonstrated on at least two formats before acceptance.
Which configuration items drive the cost of an integrated blister-cartoning line?
Cost in this category is driven by scope, not by a list price. Hoping Machinery defines its customization scope as blister size, blister materials, quantity per carton, carton specification, leaflet format, coding and inspection method, feeding method, downstream bundling, case-packing and palletizing connection, interface language, electrical component brand and data interface. Each of these items either adds or removes engineering scope, so two quotations should be normalised against the same specification sheet before they are compared. The stated minimum order quantity is one set or one complete line, and monthly capacity is 30–40 units, which is relevant when several lines are planned in one construction phase.
Can we run a material trial before shipment, and how long does an integrated line take?
Yes. The documented quality control sequence for this class of line includes a no-load trial run, a material trial, factory acceptance testing, customer witness acceptance and pre-shipment inspection, in addition to incoming material, key component, assembly and electrical safety checks. A material trial is the point at which the blister format, carton format and leaflet configuration are proven on real product rather than on a drawing. Lead time is typically 60–120 days after technical confirmation, with the final schedule subject to model, configuration, project complexity and contract terms. Buyers who want to confirm tooling material, GMP-oriented construction details and interface scope before committing can download the Hoping Machinery catalog and prepare the audit protocol in advance.
Conclusion: audit the traceability, not the adjectives
The four-layer model in this article is deliberately unglamorous. Specifications are converted into numbered claims. Documents are requested by number, standard and scope rather than by summary. The factory floor is read for machining, wiring, guarding, material identification, cleanability and stock. Acceptance is written down before the purchase order, not after it.
The DHL8005H reference case shows what a documented claim looks like when it is specific: up to 800 blisters per minute and 500 cartons per minute, a D3 intelligent top-loading parallel tracking transfer system, a three-channel servo-driven independent replenishment system, a Beckhoff motion controller with a CP9315 industrial PC, mold-change and preset-memory functions, and a stainless steel and aluminum-alloy machine structure with tooling according to technical agreement. Each of those statements can be checked, and each one should be.
An audit does not require distrust. It requires traceability. When the specification, the documents, the floor evidence and the acceptance criteria line up, the buyer is no longer choosing a brochure — it is approving a machine. For solid dosage manufacturers evaluating integrated blister-cartoning lines, that difference is the whole point of the exercise.
Next step: build your audit protocol from the source documents
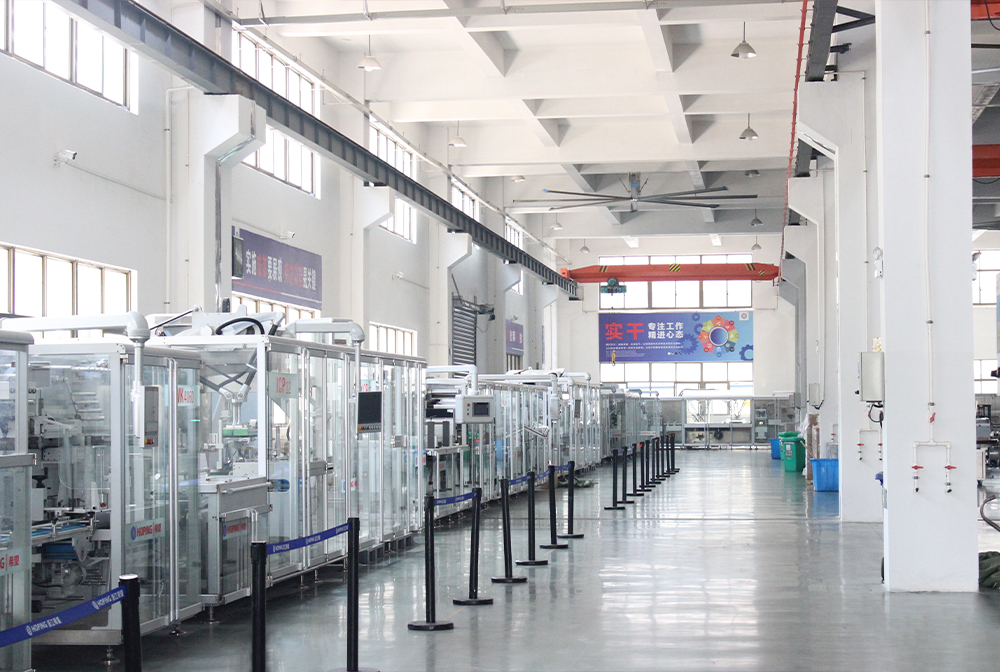
Zhejiang Hoping Machinery Co., Ltd. supplies blister packaging machines, cartoning machines, case packing machines and end-of-line packaging equipment, and supports ODM/OEM customization from blister format to downstream palletizing connection.
Download the Hoping Machinery product catalog, review the published CE and ISO certificates, and request a line configuration proposal with a documented bill of materials for your blister and carton formats.
Contact: Monica | Email: monica@xwbj.com | Tel / WhatsApp: +86 133-5610-5292 | Website: www.hopingcn.com | Address: 88th Weiwu Road, Nanbin Sub-district, Ruian City, Zhejiang Province, China.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.